CK6132 CNC Lathe: Specifications, Features and Applications
The CK6132 CNC lathe is a metal turning machine designed for machining small and medium-sized workpieces. The machine is used for turning operations and can be configured for applications such as shafts, sleeves, fasteners, hardware parts and other custom metal components.
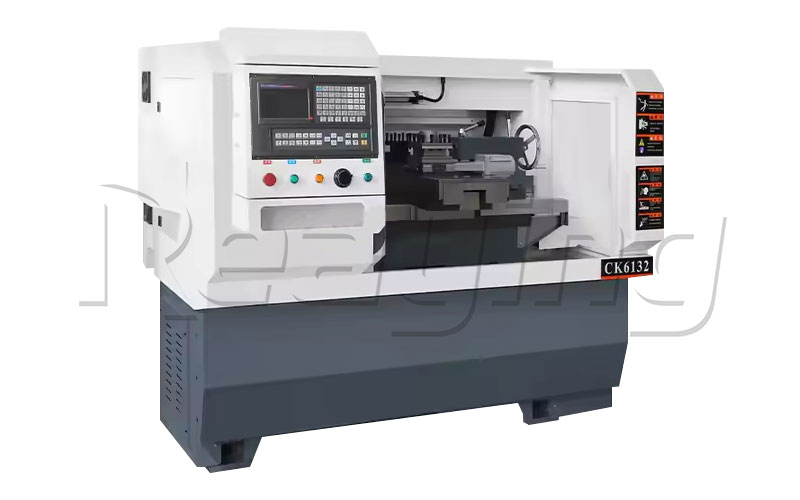
When choosing a CNC lathe, it is important to look beyond general claims such as “high precision” or “high efficiency.” The actual machine configuration, working capacity, control system, chuck, tool post and material requirements should all match the production process.
This guide explains the main CK6132 specifications, configuration, applications and key points to consider when selecting this type of CNC turning machine.
What Is a CK6132 CNC Lathe?
The CK6132 is a CNC lathe designed for metal turning.
The current Reaying configuration is identified as RY-CK6132. It uses a servo-driven main motor and is designed for turning applications involving common metal workpieces.
The standard machine configuration includes a GSK980TB3 CNC controller, pneumatic collet and gang-type tool post. Siemens 808D is available as an optional control system, while different chuck and tailstock configurations can also be customized according to production requirements.
A CK6132 CNC lathe can therefore be considered when a manufacturer needs a relatively compact CNC turning solution for repeated metal machining operations.
CK6132 CNC Lathe Specifications
The main specifications listed for the current RY-CK6132 configuration include:
| Item | CK6132 Specification |
|---|---|
| Model | RY-CK6132 |
| Function | Turning |
| Main motor | 3.7 kW servo |
| Maximum swing over bed | 320 mm |
| Maximum swing over cross slide | 130 mm |
| Maximum processing length | 400 mm |
| Spindle bore | 49 mm |
| Spindle taper | MT5 |
| Spindle head type | A2-5 |
| X-axis travel | 550 mm |
| Z-axis travel | 400 mm |
| X/Z rapid feed | 12/12 m/min |
| Standard CNC controller | GSK980TB3 |
| Optional controller | Siemens 808D |
| Standard chuck | Pneumatic collet |
| Standard tool post | Gang-type tool post |
| Standard tailstock | Without tailstock |
| Machine dimensions | 2100 × 1500 × 1700 mm |
| Weight | Approx. 1200–1300 kg |
These are the specifications currently listed on Reaying’s CK6132 product page. Configuration can vary according to customer requirements, particularly for the chuck, tailstock and CNC control system.
Key Features of the CK6132 CNC Lathe
GSK980TB3 CNC Control System
The standard CK6132 configuration uses the GSK980TB3 CNC control system.
The listed control functions include conic interpolation, ellipse interpolation, parabola interpolation, groove machining cycle functions, automatic tool compensation and custom M-code functions.
The controller also supports USB file operation and software upgrades. Siemens 808D is available as an optional control system.
The choice of CNC controller is important because it affects programming, operation and how easily the machine can be integrated into an existing machining workflow.
Pneumatic Collet Clamping
The standard CK6132 configuration uses a pneumatic collet.
According to the current product information, the pneumatic collet uses spring steel to grip the workpiece, and different inner aperture configurations can be customized for round, hexagonal and square workpieces.
Manual three-jaw, pneumatic and hydraulic chucks are also available as options.
This gives buyers more flexibility when the standard clamping arrangement does not match their workpieces.
Gang-Type Tool Post
The CK6132 uses a gang-type tool post as standard.
An electric four-station tool post is available as an option.
The appropriate tool post depends on the machining process and the number of tools that need to be used during production.
Automatic Lubrication
The machine is equipped with an electric lubrication oil pump.
The lubrication interval and lubrication duration can be adjusted according to the machine setup.
Regular lubrication remains an important part of CNC lathe maintenance because machine performance depends not only on the control system and spindle but also on the condition of the moving and mechanical components.
Tailstock Options
The standard CK6132 configuration does not include a tailstock.
Manual and pneumatic tailstocks can be selected as options.
Whether a tailstock is required depends on the type, length and stability requirements of the workpieces being machined.
What Materials Can the CK6132 CNC Lathe Process?
The current CK6132 product information lists several common metal materials, including:
- Carbon steel
- Stainless steel
- Aluminum alloy
- Copper
- Iron
The machine is intended for metal turning applications involving small and medium-sized components.
Different materials may require different cutting tools, speeds, feeds and machining strategies. Therefore, the material list should be treated as a starting point for machine selection rather than a replacement for application testing.
What Parts Can Be Machined on a CK6132?
The CK6132 is suitable for different types of rotational metal components.
The current product information specifically mentions applications involving:
- Shaft parts
- Sleeve parts
- Fasteners
- Hardware components
- Custom metal components
It is also listed for use in small and medium machinery processing, hardware processing, auto parts manufacturing and instrumentation.
This makes the CK6132 particularly relevant to manufacturers producing repeated batches of relatively small metal turning components.
What Machining Processes Does the CK6132 Support?
The CK6132 is designed primarily for turning.
The current product information lists machining processes including:
External Turning
External turning can be used to reduce the outside diameter of a workpiece and produce cylindrical surfaces.
Threading
The CNC control system can be used for programmed threading operations when the appropriate tooling and parameters are selected.
Boring
Boring is used to enlarge or finish an existing internal hole.
Grooving
Grooving tools can be used to create grooves or recessed sections according to the programmed dimensions.
Surface Finishing
Appropriate cutting tools and machining parameters can also be used for surface finishing operations.
The exact machining capability depends on the tooling, workpiece and selected machine configuration.
What Should You Consider Before Buying a CK6132 CNC Lathe?
Buying a CNC lathe should start with the workpiece rather than the machine name.
Before choosing a CK6132 configuration, check the following points.
Workpiece Size
The current CK6132 specifications list a maximum swing over the bed of 320 mm, a maximum swing over the cross slide of 130 mm, and a maximum processing length of 400 mm.
Compare these dimensions with your actual workpieces before ordering.
Spindle Requirements
The listed spindle bore is 49 mm, with an MT5 spindle taper and A2-5 spindle head.
The spindle configuration should be considered together with the diameter and type of material you normally process.
Clamping Method
The standard pneumatic collet may be suitable for many production applications, but some workpieces may require a manual three-jaw chuck, pneumatic chuck or hydraulic chuck.
Choosing the correct clamping method can help match the machine to your production process.
CNC Control
The standard GSK980TB3 system may be suitable for the intended operation, while Siemens 808D can be selected when a different control platform is required.
Before purchase, make sure the operator is familiar with the selected control system and that your existing programming workflow is compatible.
Tooling Configuration
The standard gang-type tool post and optional four-station electric tool post provide different configuration possibilities.
The best choice depends on the number and type of tools required for your normal machining jobs.
CK6132 CNC Lathe for Small and Medium Metal Parts
The CK6132 is positioned for small and medium-sized metal parts processing.
This type of machine can be useful when a production line needs to repeatedly machine components with similar turning operations rather than manually setting up every workpiece.
For example, shaft components, sleeves, fasteners and hardware parts can require repeated turning operations across multiple production batches.
The machine configuration should still be selected according to the actual dimensions, materials and processes involved.
CK6132 CNC Lathe Operation and Maintenance
CNC machining performance depends on more than the initial machine installation.
Operators should pay attention to tooling, lubrication, cleaning and CNC program management during daily production.
Keep Cutting Tools in Good Condition
A worn cutting tool can affect surface quality and dimensional consistency.
Inspect the tooling regularly and replace worn tools when necessary.
Follow the Lubrication Schedule
The CK6132 uses an electric lubrication oil pump with adjustable lubrication intervals and lubrication duration.
The lubrication system should be maintained according to the machine manufacturer’s requirements.
Check the Workholding System
The chuck or collet should securely hold the workpiece during machining.
Operators should inspect the clamping system regularly and confirm that the selected method is appropriate for the workpiece.
Check CNC Programs Before Production
Programs should be checked before running a new machining job.
For a new workpiece, it is good practice to verify dimensions, tooling, cutting parameters and the machining sequence before starting full production.
Why Test a CNC Lathe Before Buying?
A machine specification sheet provides important information, but it does not show how the machine will perform with your actual workpieces.
For this reason, buyers should prepare representative samples before making a final decision.
A practical test should cover:
- Your normal material
- Your actual workpiece dimensions
- Required turning operations
- Required tooling
- Surface finish requirements
- Dimensional requirements
- Production workflow
Testing your actual parts also helps determine whether the standard chuck, tool post and tailstock configuration are suitable.
Reaying CK6132 CNC Lathe
Reaying’s current CK6132 configuration is identified as RY-CK6132.
The machine uses a 3.7 kW servo main motor, GSK980TB3 CNC control system as standard, pneumatic collet clamping and a gang-type tool post. Siemens 808D, different chuck configurations and tailstock options are available according to customer requirements.
The current specifications list a maximum swing over bed of 320 mm, maximum processing length of 400 mm and spindle bore of 49 mm.
The machine is designed for turning common metal materials such as carbon steel, stainless steel, aluminum alloy, copper and iron, with applications including shaft parts, sleeve parts, fasteners and other metal components.
For the latest machine configuration, customers should confirm the final specifications according to their workpiece and production requirements.
CK6132 CNC Lathe After-Sales Support
The current CK6132 product information states that Reaying provides a one-year warranty, lifelong technical support, remote debugging and operation guidance.
For a CNC machine, after-sales support is an important part of the purchasing decision.
Before ordering, buyers should confirm:
- Installation requirements
- Operator training
- Remote technical support
- Spare parts availability
- Warranty terms
- CNC control support
- Machine maintenance requirements
This information should be confirmed for the specific machine configuration before purchase.
CK6132 CNC Lathe: Is It Suitable for Your Production?
The CK6132 can be considered when your production involves relatively small or medium metal components and repeated turning operations.
It may be a suitable configuration when you need:
- CNC-controlled metal turning
- Processing of shaft and sleeve parts
- Repeated production of hardware components
- Turning, threading, boring or grooving operations
- A pneumatic collet as the standard workholding configuration
- A compact CNC turning setup
The final configuration should be based on your actual workpieces, required machining operations and production volume.
Conclusion
The CK6132 CNC lathe is a CNC turning machine designed for small and medium-sized metal parts processing.
Its current configuration includes a 3.7 kW servo main motor, GSK980TB3 CNC controller, pneumatic collet, gang-type tool post and automatic lubrication system. Different chuck configurations, an optional Siemens 808D controller and optional tailstock configurations are available according to production requirements.
When selecting a CK6132, the most important factors are not simply the machine model or general precision claims. Buyers should compare the actual workpiece size, material, machining process, spindle requirements, workholding method, tooling configuration and control system.
Testing representative workpieces before purchase is also an effective way to determine whether the CK6132 configuration matches your production needs.
Need Help Choosing a CK6132 CNC Lathe?
Have a specific workpiece, material or turning requirement?
Contact Reaying with your drawings, workpiece dimensions and machining requirements so the appropriate CK6132 configuration can be evaluated for your application.
Need Help!!!
Categories
Recent Post
Tag Cloud
About Reaying
Shandong Reaying Machinery Co., Ltd. is one of the leading laser machine manufacturers around the world since 2008 with a registered capital of 3 million yuan. It is a high-tech enterprise focusing on R&D...
Read More